Showroom

Screw Conveyor
(18)
Screw Conveyors are supplied for transporting powders, granules, and bulk materials across industrial processing facilities. Featuring a rotating screw mechanism, these systems support controlled material movement through horizontal or inclined pathways. They are suitable for food processing, chemical manufacturing, agriculture, and cement industries requiring organized and consistent material handling.
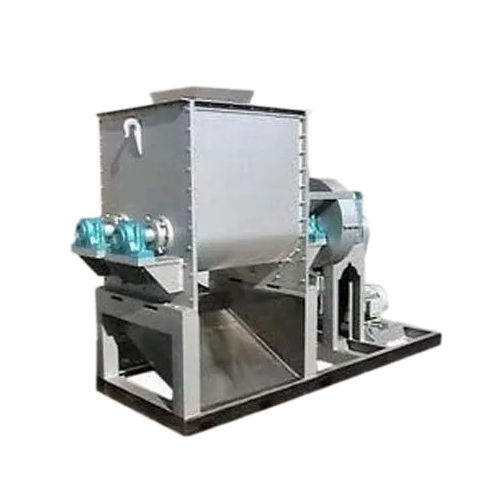
Industrial Mixer
(11)
Industrial Mixers facilitate the blending of liquids, powders, pastes, and other materials for uniform processing. Available for diverse production requirements, these machines serve chemical, pharmaceutical, food processing, and manufacturing industries. Their functional designs support efficient mixing operations, consistent product composition, and streamlined workflows across facilities handling different formulations and ingredients.
Cow Dung Dewatering System
(2)
Cow Dung Dewatering Systems help separate excess moisture from cow dung, making the material easier to handle, transport, and process. These systems are suitable for dairy farms, livestock facilities, and biogas plants. They support manure management, facilitate organic fertilizer preparation, and contribute to more organized agricultural waste processing operations.
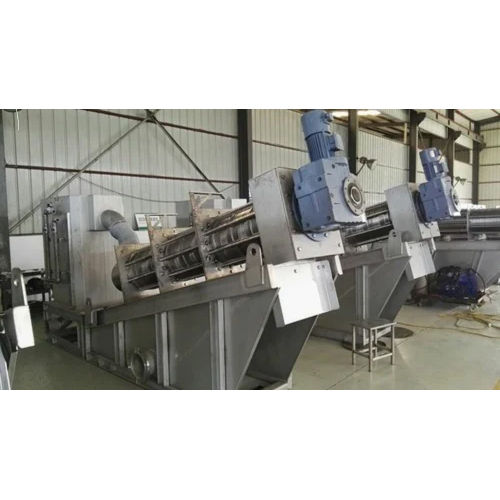
Solid Liquid Separator
(4)
Solid Liquid Separators are designed to separate suspended solids from liquids across agricultural, industrial, and wastewater treatment applications. These systems support slurry processing, effluent management, and waste reduction requirements. By facilitating effective separation, they help improve handling efficiency, recover useful materials, and simplify downstream treatment procedures in diverse operational environments.
Vibro Sifter
(2)
Vibro Sifters are used for screening powders, granules, and other materials according to particle size. Their vibrating mechanism facilitates efficient sieving across food processing, pharmaceutical, chemical, and mineral industries. Suitable for quality control and production applications, these machines help remove unwanted particles, maintain material consistency, and support organized processing operations.
Water Manifold
(2)
Water Manifolds distribute water from a common supply line to multiple outlets or connected systems. Designed for organized fluid distribution, these components are suitable for plumbing networks, industrial installations, irrigation systems, and process plants. They help simplify pipeline arrangements, facilitate controlled water delivery, and support convenient maintenance across different applications.
Pressure Vessel
(3)
Pressure Vessels are supplied for storing or processing gases and liquids under specified pressure conditions. These vessels serve chemical plants, manufacturing facilities, energy installations, and industrial processing units. Designed according to application requirements, they support controlled operations and dependable containment, with suitable construction and safety provisions essential for pressure-related applications.
Industrial Stirrer
(5)
Industrial Stirrers are utilized to agitate liquids and facilitate consistent mixing within tanks and processing vessels. Suitable for chemical production, wastewater treatment, pharmaceuticals, and food manufacturing, these systems support blending, suspension, and homogenization processes. Their application-specific configurations help maintain effective circulation and improve processing consistency across different industrial operations.
Cattle Feed Machine
(3)
Cattle Feed Machines support the preparation and processing of nutritious feed for livestock. These machines handle operations such as grinding, mixing, and feed production according to specific requirements. Suitable for dairy farms, cattle feed manufacturers, and agricultural businesses, they help streamline feed preparation while supporting consistent ingredient distribution and convenient production.
Mixer Machine
(5)
Mixer Machines are designed to combine different ingredients into a consistent mixture for manufacturing and processing applications. Available for handling powders, granules, pastes, and other materials, they serve industries ranging from food production to chemicals and construction materials. These machines help simplify blending operations and maintain uniformity across production batches.
Vibratory Separator Machine
(2)
Vibratory Separator Machines use controlled vibration to classify materials and separate unwanted particles according to size. They are suitable for screening powders, granules, liquids, and mixed materials across industrial processing environments. These machines support product quality checks, material recovery, and efficient separation, helping businesses maintain consistent processing standards throughout production.
Chain Conveyor
(3)
Chain Conveyors facilitate the movement of heavy loads, components, and bulk materials along defined production routes. Their chain-driven mechanism makes them suitable for manufacturing plants, warehouses, assembly lines, and industrial handling facilities. These systems support continuous material transfer, organized workflow management, and dependable transportation in applications involving demanding operating conditions.
Stationery Mixture
(2)
Stationery Mixtures are used for blending materials in applications requiring consistent mixing and uniform distribution of ingredients. Suitable configurations can support manufacturing processes involving powders, granules, and other compatible materials. These machines help streamline batch preparation, simplify material handling, and maintain production consistency across facilities with specific mixing requirements.
Wire Mesh Belt Conveyor
(2)
Wire Mesh Belt Conveyors are designed to transport products through production, drying, cooling, and processing stages. Their open mesh construction allows airflow and drainage where required, making them suitable for food processing, heat treatment, and industrial manufacturing. These conveyors support continuous movement and efficient product handling across specialized production lines.
Biomass Pyrolysis Plant
(2)
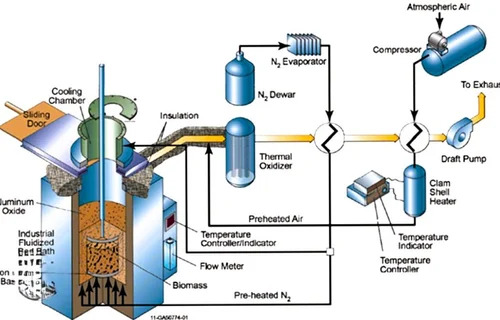
Biomass Pyrolysis Plants process organic materials through thermal decomposition under controlled oxygen-limited conditions. These plants can convert suitable biomass into products such as biochar, condensable liquids, and combustible gases, depending on feedstock and operating parameters. They serve agricultural waste processing and biomass utilization projects focused on resource recovery and waste management.
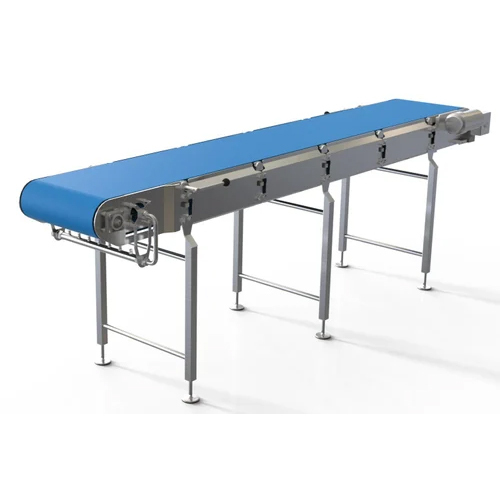
Industrial Conveyor
(5)
Industrial Conveyors are supplied for transporting materials and products between different operational stages. Available in various configurations, these systems support manufacturing, packaging, warehousing, mining, and processing applications. They help reduce manual material movement, organize production workflows, and maintain steady transportation across facilities handling diverse loads and operational requirements.
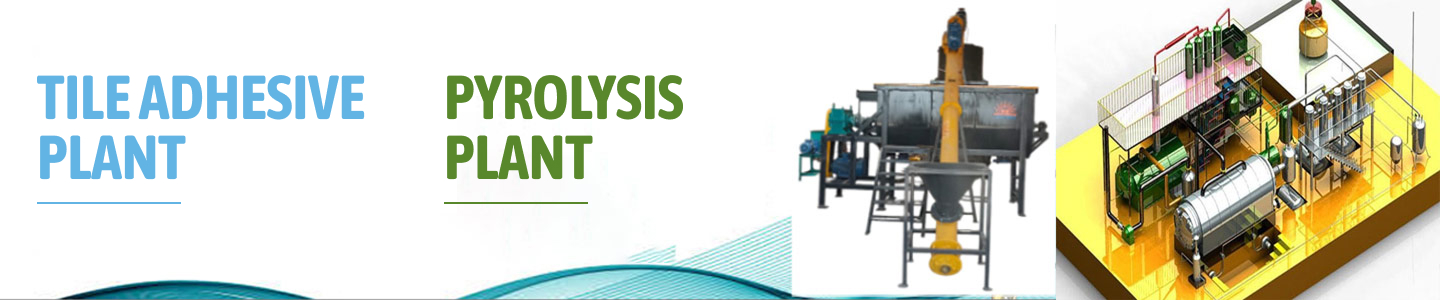
Tile Adhesive Plant
(3)
Tile Adhesive Plants are designed for manufacturing dry-mix adhesive products used in tile installation and construction applications. These plants typically integrate material feeding, batching, mixing, and packaging operations. Suitable for building material manufacturers, they support consistent formulation, organized production, and efficient handling of cement-based powders and other compatible ingredients.
Chemical Mixing Bagging Plant
(4)
Chemical Mixing Bagging Plants combine material blending and packaging operations within an integrated production setup. Designed for suitable chemical powders and granules, these plants support batch preparation, controlled material handling, and organized bag filling. They serve chemical manufacturers seeking coordinated processing workflows, consistent product distribution, and efficient packaging operations.
Bag Sealing Machines
(2)
Bag Sealing Machines are used to close filled bags securely across packaging and dispatch operations. Suitable for different compatible packaging materials, these machines serve food processing, agriculture, chemicals, and manufacturing industries. They support neat package closure, help protect contents during handling, and facilitate efficient packaging workflows across varied production environments.
Adhesive Making Plant
(6)
Adhesive Making Plants support the preparation and processing of adhesive formulations for industrial and commercial applications. Depending on the formulation, these plants may include mixing vessels, heating arrangements, dosing systems, and other processing equipment. They serve adhesive manufacturers requiring controlled ingredient blending, consistent batch preparation, and organized production operations.
Waste Tyre Recycle Plant
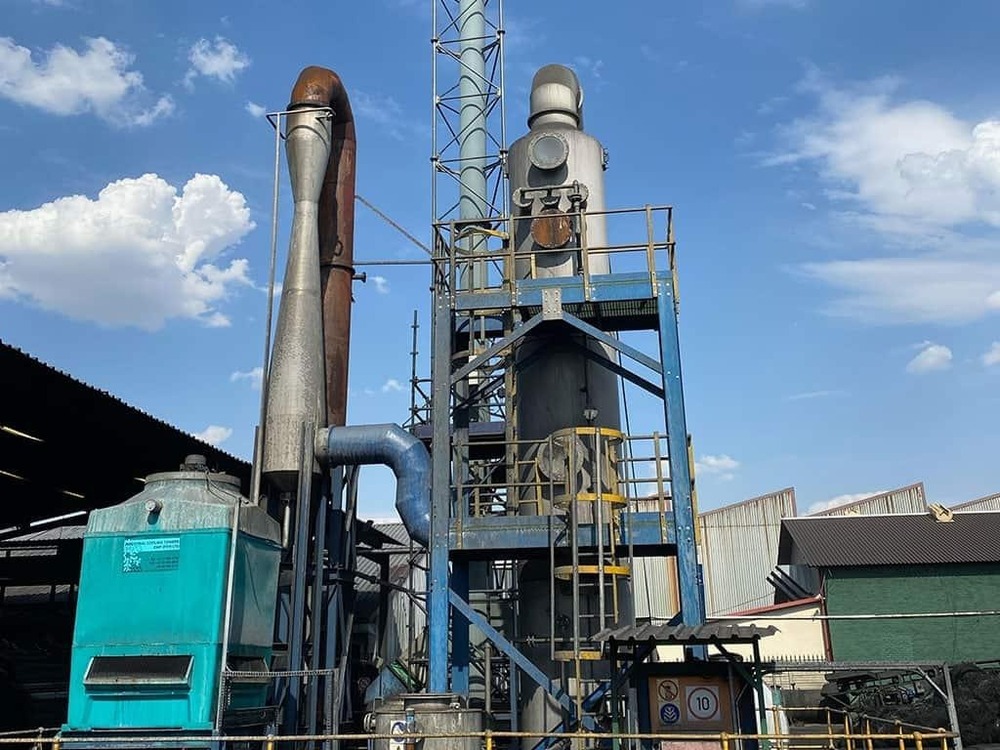
(10)
Waste Tyre Recycle Plants process discarded tyres to recover reusable materials and support waste management initiatives. Depending on the technology used, outputs may include rubber granules, recovered steel, textile fractions, or pyrolysis products. These plants serve recycling businesses and industrial operators seeking practical solutions for tyre waste processing and resource recovery.
Sigma Mixer
(2)
Sigma Mixers are designed for intensive kneading and blending of viscous materials, dough-like compounds, and thick pastes. Featuring specially shaped mixing blades, these machines support applications in rubber, chemicals, adhesives, pharmaceuticals, and related industries. They facilitate thorough material incorporation and consistent batch processing for formulations requiring high mixing force.
Pyrolysis Plant
(3)
Pyrolysis Plants use controlled heating in an oxygen-limited environment to break down suitable feedstocks into different recoverable products. Depending on the input material and system design, outputs may include oil, gas, and solid char. These plants serve waste processing and resource recovery applications, with operating controls and emission management suited to the feedstock and applicable regulations.


Back to top